Hot & Cold Thermal Bags, Insulated Mailers & Cold Chain Delivery Packaging

Fertilizer, Pesticide & Agrochemical Packaging

Cleaner, Laundry & Air Care Packaging

Custom Medical Packaging Solutions

Protective Structures, Inserts and Retail Packs

Custom Protein Powder Pouches, Vitamin Stick Packs & Nutrition Bar Bags

Cosmetics, Fragrance and Skincare Packaging

Takeout, Bakery and Beverage Packaging

Kibble, treat & wet food packaging

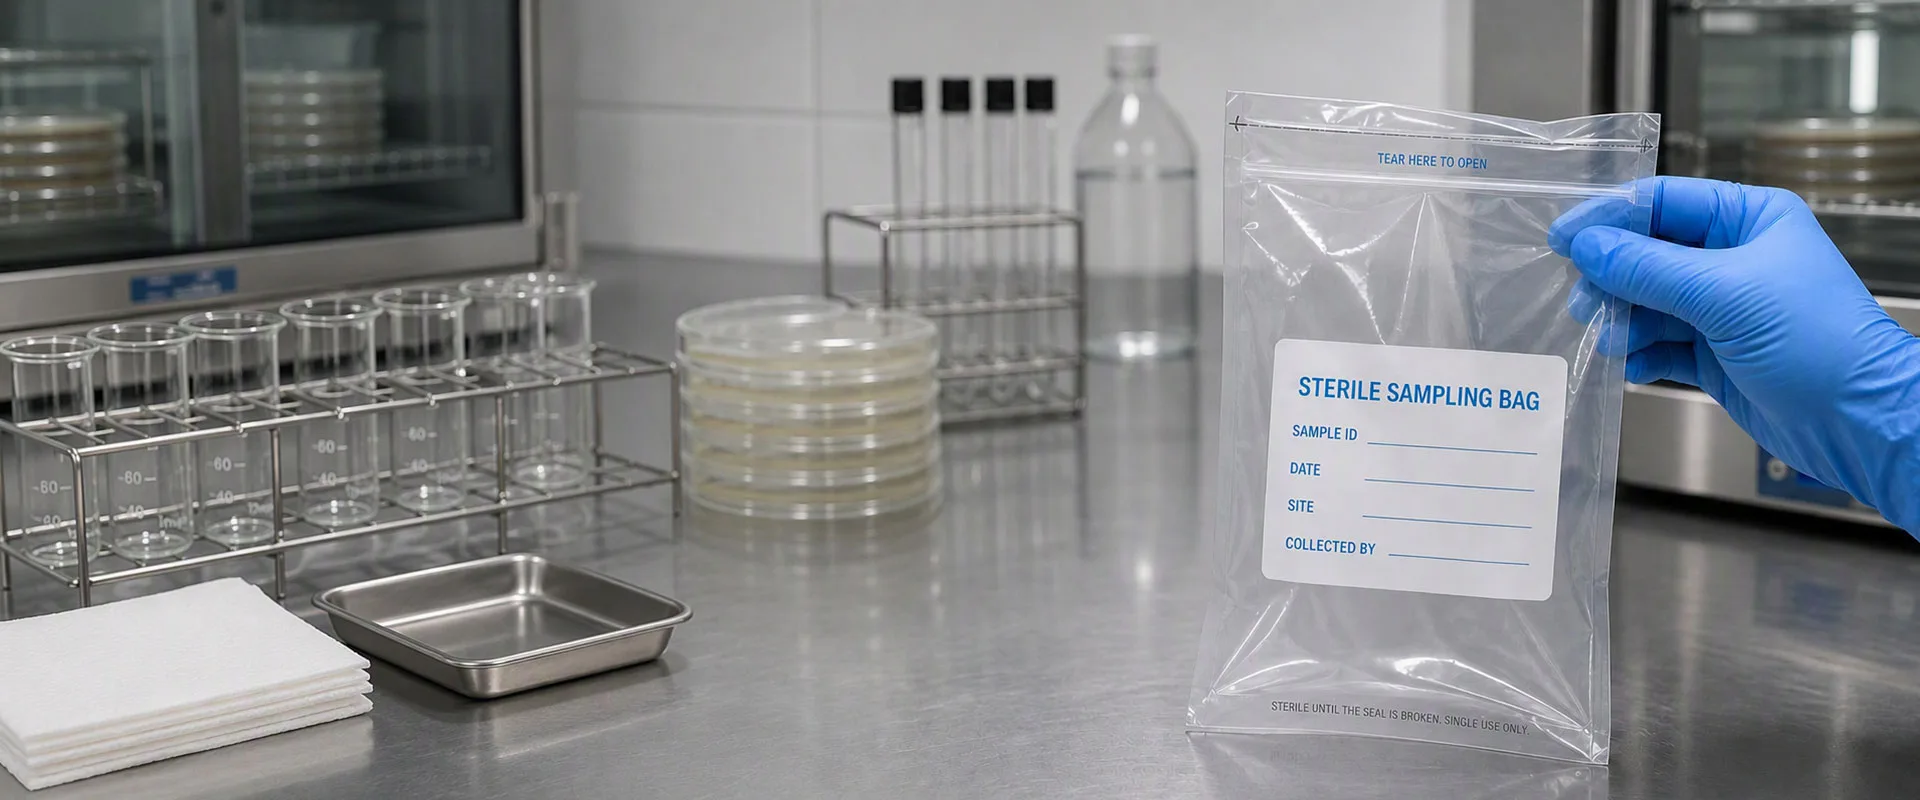
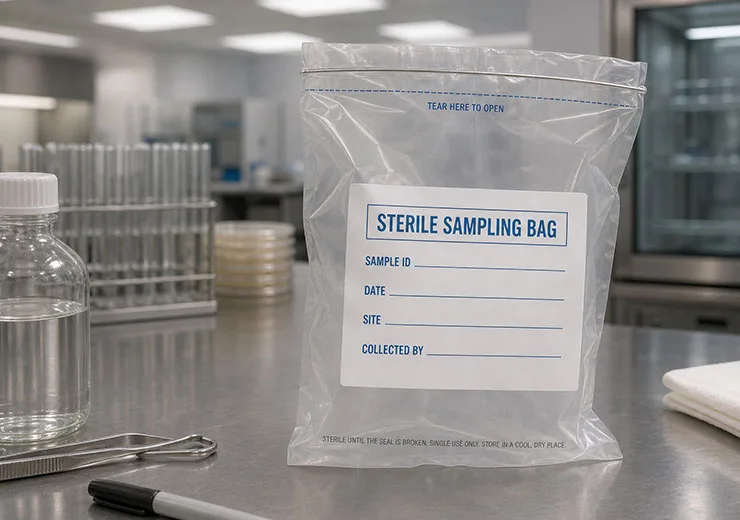
As a sterile pouch manufacturer and pharmaceutical packaging supplier serving Class I–III medical device makers, contract manufacturers, and pharma brands in 40+ countries, we understand packaging is an integral part of the regulated product. Our medical-grade flexible packaging solutions are purposefully designed to solve the toughest barrier, sterilization, and audit challenges, ensuring a secure and efficient path to market.
Sterile barrier. Fortress protection. Audit-proof compliance — engineered for pharmaceuticals that demand zero risk from factory to patient.
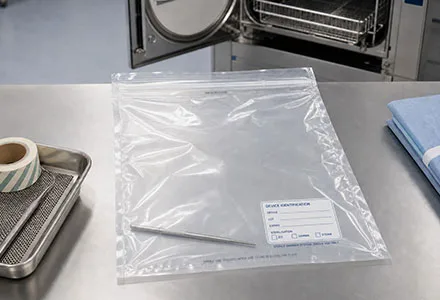
Our Tyvek and medical paper pouches strictly comply with ISO 11607-1, validating a Sterility Assurance Level (SAL) of 10⁻⁶ from sterilization to the point of use.
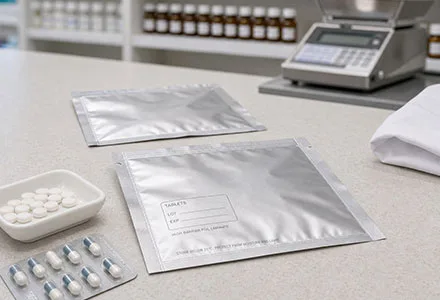
Our aluminum foil pharma pouches deliver an ultra-high barrier (WVTR < 0.01 g/m²/day) and UV-blocking opaque films to protect active pharmaceutical ingredients (APIs).
Every batch is manufactured under GMP controls with full material traceability, supporting your FDA 21 CFR 820 and EU MDR submission timelines.
Every medical product — from a sterile scalpel to a moisture-sensitive oral tablet — has an optimal pouch format defined by its sterilization method, barrier requirement, and regulatory classification. As an OEM medical packaging manufacturer with in-house multi-layer lamination and cleanroom-controlled converting, we are fully equipped to fulfill your custom flexible packaging requirements across all dimensions and specifications. Below is our complete capability matrix.
Zero cross-contamination. Zero sterilization risk. Zero labeling steps — engineered for medical and pharma products that demand absolute compliance from fab to patient.
Physically separated converting zone with HEPA-filtered air. Food and medical lines never run concurrently to prevent cross-contamination.
Materials pre-qualified for EO (ISO 11135), Gamma (ISO 11137), and Steam (ISO 17665) with aeration-safe, non-fading buried inks.
ISO 9001 certified quality system; materials qualified for FDA 21 CFR 820 and EU MDR compliance support; partner audits supported on request.
Clear answers about medical & pharmaceutical packaging, customization, pricing, shipping and after-sales support.
Yes. Every batch ships with full batch records, COAs, and sterilization validation summaries to directly support your QA team’s compliance files.
Yes. We support clinical trial runs with flexible order quantities evaluated per project, complete with serialization and unique random ID printing.
We conduct 100% visual inspection and sampling dye-penetration tests (ASTM F1929). Our peel strength is strictly documented between 0.5–4.0 N/15mm (ASTM F88).
INQUIRY