Custom packaging ·7-day sampling - Global delivery support
Liquid Beverage Stand-up Pouch with Gusseted Leak-Proof Base and Tamper-Evident Spout Cap for Juice and Drinks

Liquid Beverage Stand-up Pouch with Gusseted Leak-Proof Base and Tamper-Evident Spout Cap for Juice and Drinks

The liquid beverage stand-up pouch represents the most mechanically demanding format in the flexible packaging portfolio because it must contain a product that exerts hydrostatic pressure — uniform force distributed across every interior surface, proportional to the height of the liquid column — rather than the localized, gravity-concentrated loads of solid products. This fundamental distinction in loading mode means that every seal, gusset fold, and spout attachment point on a liquid pouch must be designed for the pressure condition, not just the product weight.

Color

Size

  • 200ml
  • 250ml
  • 300ml
  • 350ml
  • 500ml
  • Custom Size Available

Shipping

Express (DHL/FedEx/UPS), Sea Freight, Air Freight

Payment Terms

T/T (Bank Transfer), L/C at Sight, PayPal, Western Union, Alibaba Trade Assurance

Lead Time

Samples: 3-5 working days | Mass Production: 15-25 working days

Samples

Contact us for FREE samples
Contact Us WhatsApp

Product Description

PP-g-MAH Tie Layer for Spout Seal and Tamper-Evident Cap

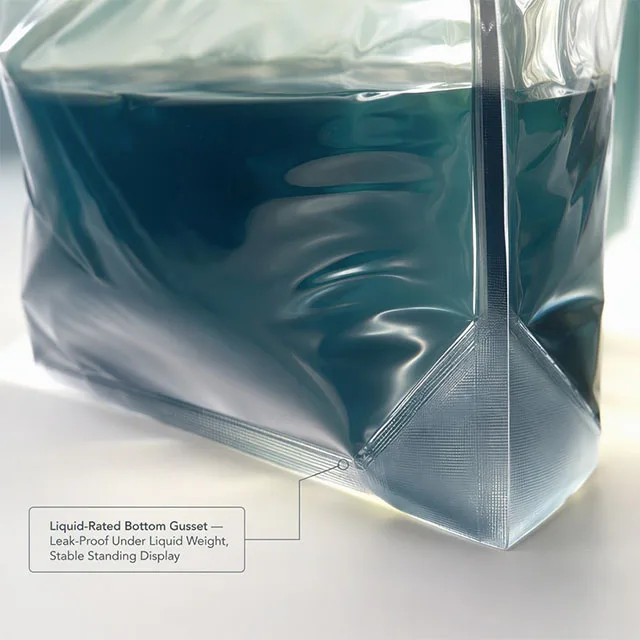
The gusseted bottom seal is the critical structural element that makes a liquid stand-up pouch possible. When the pouch is filled with 250-500ml of liquid, the hydrostatic pressure at the base is approximately 1.5-2.5 kPa (0.015-0.025 atm) above ambient — a seemingly modest number that translates to a distributed force of 30-50 Newtons across the 200cm² bottom panel area. This continuous outward pressure would, in a flat-sealed pouch, progressively peel open the bottom seal from the inside through a creep-failure mechanism. The gusset geometry solves this by folding the bottom film inward, creating a W-shaped cross-section where the outward pressure actually compresses the fold against itself — the higher the internal pressure, the tighter the gusset fold seals. This self-reinforcing behavior is unique to gusseted liquid packaging and is the reason it requires no additional structural support to stand independently on retail shelves.

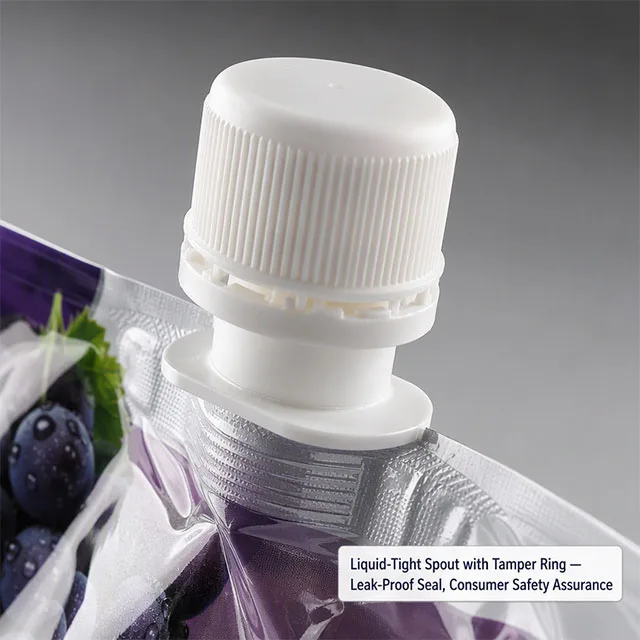
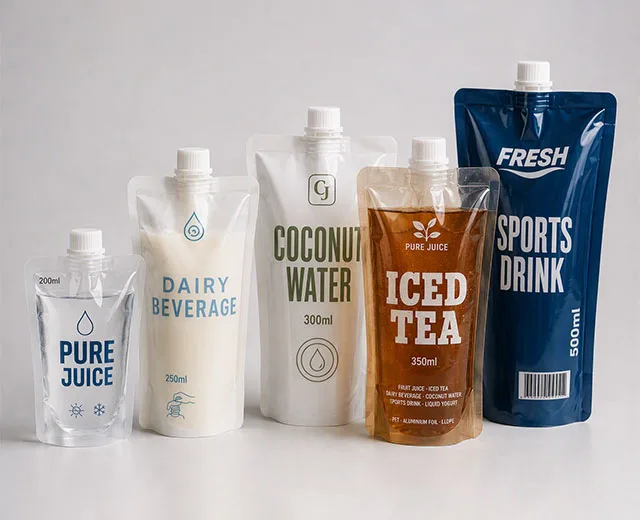
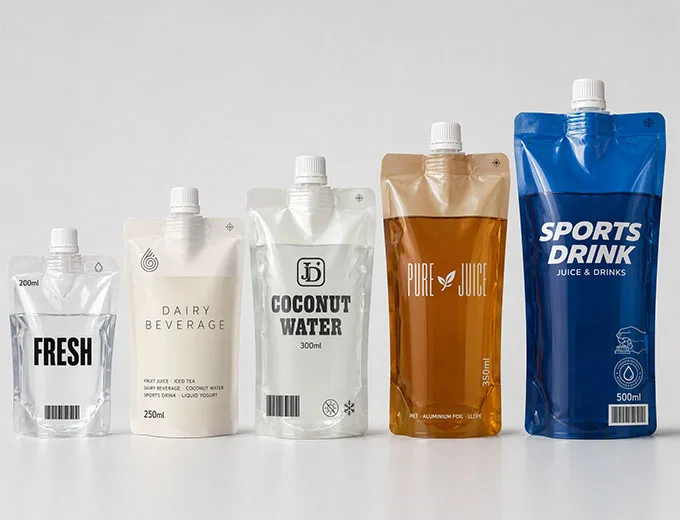
The spout fitment — injection-molded from polypropylene — is inserted between the top film layers and heat-sealed during pouch forming. The seal between the spout’s PP flange and the PE inner layer of the film requires a specialized PP-g-MAH (maleic anhydride grafted polypropylene) tie layer that creates covalent bonds across the PP-PE interface — a materials compatibility challenge that cannot be solved by heat and pressure alone because PP and PE have different melting points and are thermodynamically immiscible. The tamper-evident cap uses a breaking-bridge design: a ring of plastic bridges around the cap base must fracture visibly when the cap is twisted open for the first time, providing irrefutable evidence of prior opening. The bridges are engineered with a fracture torque of 1.5-2.5 N·m — low enough for comfortable one-hand opening, high enough to survive the vibration and compression of distribution without accidental breakage. Key applications: fruit juices, iced teas, dairy-based beverages, coconut water, sports drinks, and liquid yogurt.

Product Description

Specifications

Customizable Color & Size Options for Every Market Need
Color Size
Transparent 200ml
Soft White 250ml
Pearl White 300ml
Amber Tint 350ml
Ocean Blue 500ml
Custom Color Available Custom Size Available

Printing Process

Dedicated Spout Registration and Soft-Touch Wet Grip Coating
Printing Process

Printing on liquid beverage stand-up pouches operates under a constraint unknown to dry-product packaging: the optical distortion introduced by the liquid contents. When light passes through the front film, through the liquid, reflects off the back film, and passes back through the liquid and front film to reach the consumer’s eye, the refractive index of the liquid shifts the apparent position and color of the printed image. This effect is most pronounced with transparent pouches containing clear liquids (water, coconut water) where the distortion is minimal, and with opaque pouches (pearl white, foil laminate) where the distortion is eliminated entirely — the worst case is a translucent liquid behind a semi-transparent film, where the color cast of the liquid (amber tea, purple grape juice, orange mango) shifts the perceived color temperature of everything printed above it.

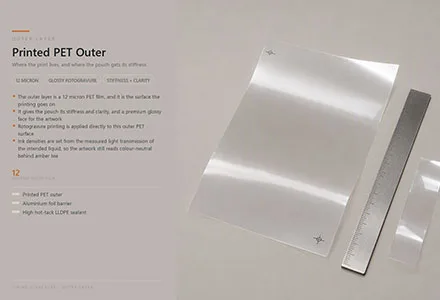
Our rotogravure printing on the outer PET surface compensates for this effect through a color management workflow that models the spectral transmission of the intended liquid fill and adjusts ink densities pre-press. For example, a pouch intended to hold amber-colored iced tea receives a 5-8% boost in cyan and yellow ink densities to counteract the warm color cast of the liquid behind it, ensuring the printed graphics appear color-neutral to the consumer. This compensation is product-specific and is calculated using spectrophotometric measurements of the actual liquid product through the actual film structure.

The spout area presents a unique registration challenge: because the spout is a rigid object embedded in flexible film, the film around the spout flange cannot stretch or shift during the printing-to-pouch-forming process without creating alignment errors between the printed graphics and the physical spout position. We solve this through a dedicated spout-area registration mark — separate from the main color-to-color registration marks — that is scanned by the pouch-making machine’s vision system immediately before spout insertion, adjusting the spout placement servo ±1.5mm in real time to center the spout within its printed target zone. The print finish in the hand-grip area above the liquid fill line uses a soft-touch matte coating — a water-based polyurethane dispersion applied as the final print station — that increases the coefficient of friction for secure grip when the pouch surface is wet with condensation.

Lining Decoration

Outer Layer

Outer Layer

High Hot-Tack LLDPE
Middle Layer

Middle Layer

Aluminium Foil Core
Contact Layer

Contact Layer

Printed PET Outer

The inner lining of a liquid beverage pouch must overcome the single greatest challenge in liquid flexible packaging: preventing delamination at the seal interface when the sealant is in continuous contact with a liquid that contains surfactants, acids, and essential oils — all of which can act as interfacial agents that weaken the cohesive strength of heat seals over time. This phenomenon, known as “seal creep failure under chemical stress,” is the leading cause of liquid pouch leakage in the field and is notoriously difficult to detect through standard QC burst testing, which applies instantaneous pressure rather than the sustained low-level stress of long-term liquid contact.

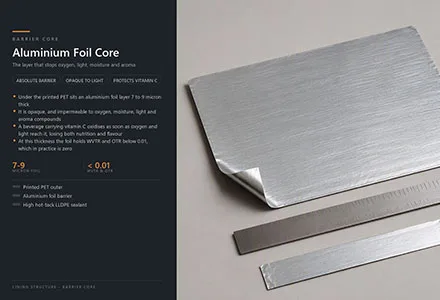
The film structure begins with an outer printed PET layer (12μm) that provides stiffness, clarity, and a premium glossy surface for high-definition rotogravure printing. Beneath this, an aluminum foil layer (7-9μm) serves as the absolute barrier — opaque, impermeable to oxygen, moisture, light, and aroma compounds. The foil is essential for beverage products containing vitamin C (ascorbic acid), which oxidizes rapidly in the presence of oxygen and light, causing both nutritional degradation and the development of off-flavors. A 7μm foil layer provides WVTR and OTR values below 0.01 units — effectively zero for practical purposes.

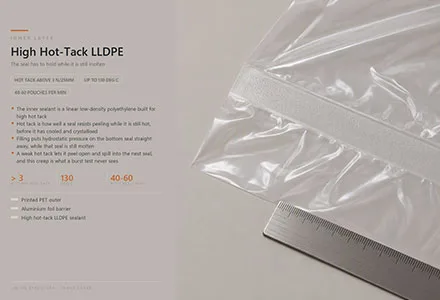
The inner sealant is a specialized linear low-density polyethylene (LLDPE) formulated with a high hot-tack strength — the ability of the molten seal to resist peeling forces while still hot, before it has cooled and crystallized. This property is critical because liquid-filled pouches exert immediate hydrostatic pressure on the still-molten bottom seal during the filling operation. If the hot-tack strength is insufficient, the seal peels open before it solidifies, and liquid product spills into the sealing area, contaminating subsequent seals in a cascading failure. Our LLDPE sealant maintains hot-tack strength above 3 N/25mm at temperatures up to 130°C, providing a processing window wide enough for reliable high-speed operation at 40-60 pouches per minute.

Get In Touch With Us

Reach out for any inquiries, support, or to discuss how we can meet your industrial needs.
  • Address

    North Side Of Nanyi Road, Shiwan Town Science And Technology Park (10th Floor, Building 1, No. 13)

Contact Me

    You can upload a PDF or an image(max 5MB)

    INQUIRY