Mailer complaints rarely arrive as complaints. They arrive as a soft ice pack or a seam split at the customer’s door, after the fault has been repeated a few thousand times. Four checks on a sample, run before the lot is released, catch what causes them.
Four checks, one sample bag
Take a bag from the carton, keep it flat, and work through four points: the three welded edges, the foam behind each face, the two closures at the mouth, and which ply faces the goods. Do them in that order – the weld check eliminates a bad bag fastest, and the ply check needs a bag cut open.
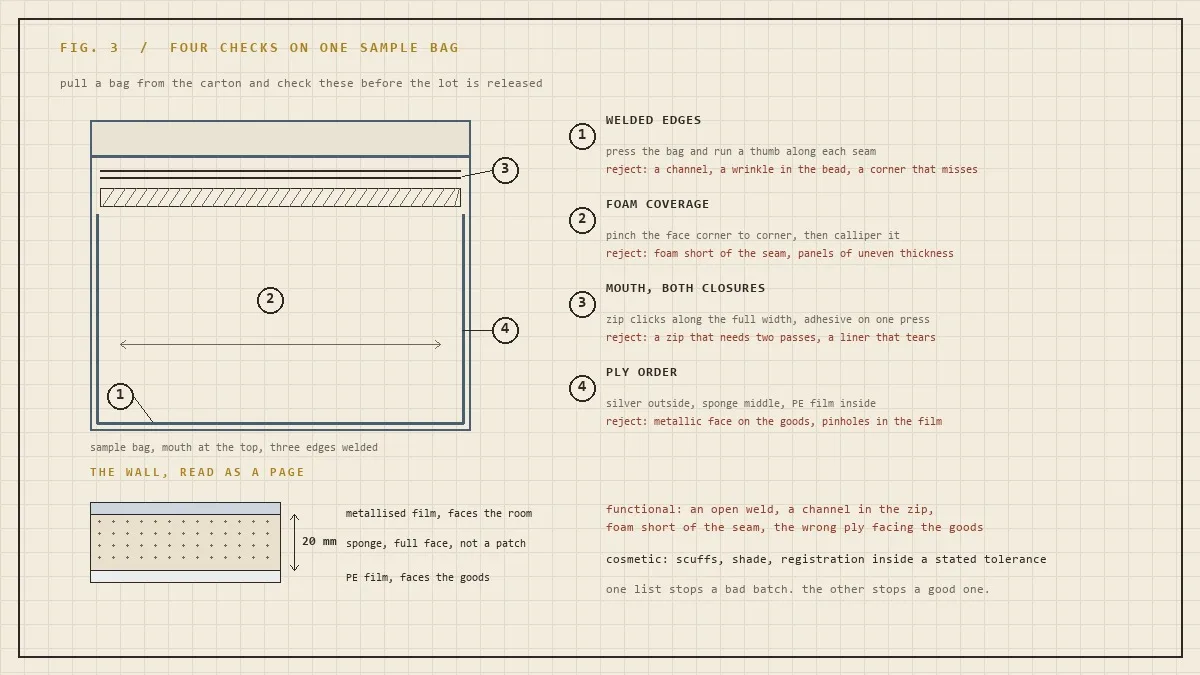 Fig.3 Four points to check on one flat sample bag, and the wall read layer by layer
The count has a standard behind it. ISO 2859-1 is the scheme most buyers write into a purchase order: pick an inspection level, usually general II, and lot size gives you a sample size and an acceptance number. AQL 2.5 for major defects and 4.0 for minor is a common pairing; confirm it with your quality team first.
A supplier never asked for sample size and AQL inspects by feel: a first batch that is fine, a fifth that is not.
Check one: the three welded edges
Every edge but the mouth is welded, and the weld fails first. Press the bag so it holds air and run a thumb along the bottom and both sides: you want a continuous bead, full width, no channel where the plies failed to bond.
On a printed bag, a dull grey line along the seam means heat reached the ink and crazed the metallised layer, which is why the artwork keeps a clear margin along every weld.
Reject a wrinkle caught in the bead, a bead that narrows to half width, a corner where a side seam misses the bottom one. Bend one sample until the corner peels; that tells you more than fifty perfect-looking bags.
Check two: foam that runs the full face
Twenty millimetres of sponge is worth twenty only if it covers the panel. Pinch the face corner to corner: resistance at the corner should match the middle. A patch bonded to the centre feels right in the hand and protects nothing at the edge, where a carton corner lands.
Measure with a calliper at three points per face. A
vacuum-compressed EPE foam mailer ships pressed flat on purpose: let the sample recover first, or you will reject a bag doing what it was built to do.
Reject foam that stops short of the seam, uneven panels, or a face still short after ten minutes.
Check three: the mouth has to close twice
The mouth closes twice: a two-rib zip, and above it an adhesive strip under a peel-off liner that folds onto the face below the zip. Check them separately: either can pass while the other fails.
Zip: drag a fingernail along the closed ribs end to end. Both should click and stay shut; a section that opens under a light pull is a channel, and a channel is a hole. Adhesive: peel the liner on five bags, press the flap down once as a packer would, then open it again. The strip should hold and should not lift the print it was pressed onto.
Check four: which ply faces the goods
On a reflective mailer the ply order is the specification: metallised film outside, sponge in the middle, plastic film inside. Nothing metallic should face the load, because a foil face scuffs a printed carton and the weld closes on the film, not on the foil.
Cut the sample open and read the layers like a page. If the silver is inside, the bag was built wrong and no care at the packing line will fix it. Hold the foil face to a light as well: pinholes show as bright specks, and one turns a reflective bag into a plain one. The reasoning is in
the three paths heat takes into a parcel.
Reject the fault, not the finish
A silver mailer scuffs, creases where folded, and its sheen varies across a stack. None of that changes performance, and a spec that rejects it will reject every batch you receive. A
metallised foil insulated mailer is judged on what the layers do, not on how evenly they shine.
Keep two lists. Functional: an open weld, a channel in the zip, foam short of a seam, the wrong ply facing the goods, a pinhole. Cosmetic: scuffs, registration, shade under warehouse light, each with a tolerance written down, because ‘looks right’ is where arguments start.
One list stops a bad batch leaving; the other stops a good one being rejected, and a rejected batch misses its sailing with the freight booked. If freight is the number you chase,
what flat-packing changes about the bill is the other half.
Send us the checks you want run and the AQL you work to; we run them on the pre-production sample and on the finished lot, with a photograph of each point.
Ask for the inspection sheet